Trade Insights
Pre-Shipment Inspection: A Checklist for International Buyers
A pre-shipment inspection helps international buyers verify whether goods, packaging, quantities, and shipping marks conform to the purchase order before the supplier dispatches the cargo. The inspection should occur when production is complete and enough goods are packed to permit representative sampling. Buyers should define the inspection scope, sampling method, acceptance criteria, and reporting requirements in writing before production begins.
What is a pre-shipment inspection?
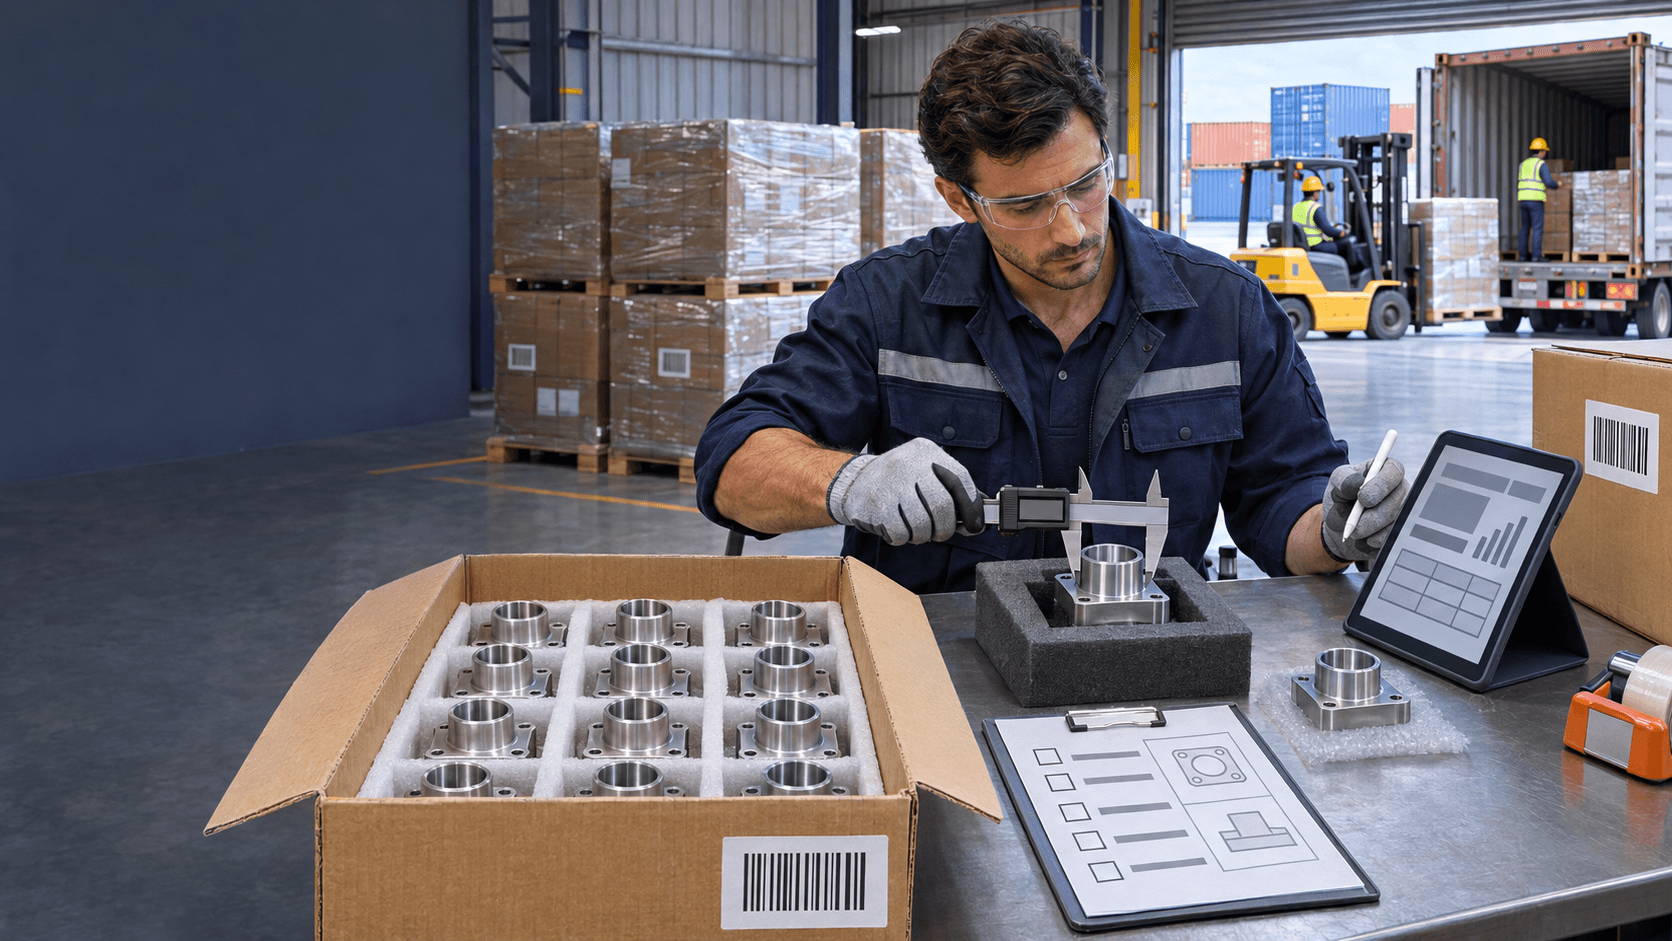
A pre-shipment inspection, commonly abbreviated as PSI, is a structured examination of goods before they leave the supplier’s facility. An inspector selects samples from the finished order, checks them against approved specifications, documents defects, and reports whether the inspected lot meets the buyer’s defined requirements.
PSI is a risk-control measure rather than a guarantee. It examines a sample at a particular point in time and cannot confirm the condition of every unit, prevent all transport damage, or replace appropriate supplier qualification and contract terms.
When should the inspection take place?
The inspection should normally be scheduled after production is complete and most of the order has been packed, but before the goods are loaded or released for shipment. Inspecting too early creates a risk that unfinished or unexamined goods will be added later. Inspecting after dispatch removes much of the buyer’s ability to require correction before the cargo leaves the supplier.
The buyer should confirm the following before sending an inspector:
Production is complete.
The goods are available at the stated inspection location.
Finished units and export cartons can be accessed and opened.
Approved samples, specifications, and testing instructions are available.
The supplier has enough time to correct problems before the planned shipment date.
What documents should the buyer prepare?
An inspector can only evaluate requirements that are clear and measurable. The inspection file should therefore convert the commercial agreement into an operational checklist.
Document or reference | What it should define |
|---|---|
Purchase order | Product references, quantities, variants, agreed packaging, and delivery terms |
Technical specification | Materials, dimensions, tolerances, performance requirements, and workmanship standards |
Approved sample | Accepted appearance, construction, colour, finish, and functionality |
Packaging specification | Unit packaging, carton construction, assortment, protection, sealing, and pallet requirements |
Artwork and label files | Branding, product information, barcodes, warnings, symbols, and shipping marks |
Inspection standard | Sampling plan, defect categories, acceptance limits, and decision rules |
Testing instructions | Required on-site checks, equipment, sample sizes, methods, and pass criteria |
What should a pre-shipment inspection checklist cover?
1. Order identity and inspection conditions
Confirm the supplier, factory, inspection address, purchase order, and product references.
Record the production completion and packing status.
Check whether all ordered variants are present.
Confirm that samples were selected by the inspector rather than prepared in advance by the supplier.
Record any restricted access, missing equipment, or conditions that limited the inspection.
2. Quantity verification
Count finished units, inner packs, master cartons, and pallets where applicable.
Compare available quantities with the purchase order and packing list.
Verify the distribution of sizes, colours, models, grades, or batch references.
Record incomplete, unpacked, rejected, or unavailable quantities separately.
3. Product specifications
Compare product construction and materials with the approved specification.
Measure critical dimensions and apply the agreed tolerances.
Check weight, colour, finish, components, and accessories where relevant.
Confirm model numbers, batch codes, and other product identifiers.
Photograph measurements and significant observations.
4. Workmanship and visual defects
Inspect for cracks, deformation, contamination, corrosion, scratches, stains, sharp edges, loose parts, or poor assembly.
Check consistency across the selected samples.
Separate defects into critical, major, and minor categories according to the buyer’s written definitions.
Record each defect with a clear description, quantity, and photograph.
5. Function and performance
Perform the agreed functional checks on selected units.
Test moving parts, controls, fittings, connections, or assembly procedures as applicable.
Verify that included accessories and instructions allow the product to be used as intended.
Record test conditions, sample sizes, results, and any equipment used.
6. Packaging and protection
Confirm unit-pack, inner-carton, and master-carton quantities.
Check packaging materials, carton dimensions, sealing, and protective components.
Assess whether products are adequately separated and immobilised inside the carton.
Inspect cartons for moisture, crushing, punctures, contamination, or weak closures.
Verify pallet configuration and protection if palletisation is part of the order.
7. Labels, barcodes, and shipping marks
Compare printed content with the buyer-approved artwork.
Check product references, quantities, batch identifiers, and destination marks.
Verify barcode content and scan selected labels where suitable equipment is available.
Confirm that labels are legible, correctly positioned, and securely attached.
Check that required warnings and handling symbols match the buyer’s documented requirements.
8. Basic on-site tests
On-site tests depend on the product. They may include assembly, operation, dimensional measurement, weight checks, carton-drop checks, barcode scanning, or simple packaging assessments. Each test must have a defined method and pass criterion.
Laboratory testing may still be necessary for chemical composition, material identity, electrical safety, food safety, or other characteristics that cannot be reliably verified at the factory. A basic PSI should not be presented as laboratory confirmation.
9. Export documentation consistency
Compare product descriptions and quantities across the available commercial documents.
Check whether carton counts, weights, dimensions, and marks are internally consistent.
Confirm that the goods inspected correspond to the items intended for shipment.
Escalate inconsistencies before documents are finalised and cargo is released.
How should buyers define sampling and defect limits?
Checking every unit may be impractical, so many inspections use statistical sampling. The buyer should specify the sampling standard, inspection level, lot size, and acceptance limits in the purchase agreement or quality plan. These instructions determine how many units are examined and how observed defects affect the result.
Defect definitions should be tailored to the product:
Critical defect: A condition that may create an unacceptable safety risk or make the product unsuitable for its intended use.
Major defect: A problem likely to cause product failure, materially reduce usability, or lead a reasonable buyer to reject the item.
Minor defect: A limited departure from the specification that does not materially affect normal use but still falls below the agreed standard.
Classification should not be left to interpretation on inspection day. Buyers should provide product-specific examples, photographs, and limits before production.
What should the inspection report contain?
A useful report should enable a commercial decision without requiring the buyer to reconstruct what happened at the factory. It should include:
Supplier, location, date, purchase order, and inspected product references
Ordered, completed, packed, available, and inspected quantities
Sampling method and number of samples examined
Specification, measurement, and test results
Defects by category, with counts and photographs
Packaging, labelling, barcode, and shipping-mark findings
Any deviation from the inspection instructions
A clear result based on the buyer’s predefined criteria
The report should distinguish observed facts from recommendations. The inspector reports findings; the buyer retains responsibility for the commercial decision to approve, reject, rework, or reinspect the order.
What should the buyer do after a failed inspection?
Place shipment on hold. Do not release the balance payment or authorise dispatch until the findings are reviewed.
Identify the affected scope. Determine which products, batches, cartons, or requirements failed.
Request a corrective-action plan. The supplier should explain how defective goods will be identified, corrected, and prevented from re-entering the shipment.
Require evidence. Ask for updated production records and photographs, but do not rely on supplier-selected evidence when the risk is significant.
Arrange reinspection. A new inspection can verify corrections using independently selected samples.
Document the decision. Record any concession, replacement, price adjustment, delayed shipment, or rejection in writing.
A conditional result should not automatically be treated as approval. The buyer must evaluate whether the deviation affects safety, usability, compliance, customer expectations, or downstream production.
Which mistakes reduce the value of pre-shipment inspection?
Booking the inspection before the order is substantially complete
Using vague specifications or relying only on verbal agreements
Allowing the supplier to select inspection samples
Defining defect limits after defects have already been found
Checking appearance while omitting function, packaging, or quantity
Treating a sampled inspection as a guarantee for every unit
Releasing payment before reviewing the full inspection report
Accepting rework without independent verification when the risk is material
How can Hoorban support the inspection process?
Hoorban approaches sourcing and trade through the combined use of management expertise, experience from Iran’s commercial ecosystem, current knowledge, and artificial intelligence. Within a sourcing or import process, Hoorban can help buyers organise product requirements, supplier information, commercial documentation, and inspection criteria so that the pre-shipment decision is based on clearly documented expectations.
The precise scope should be agreed for each transaction, including product specifications, inspection location, required checks, reporting format, and responsibility for the final release decision.
Frequently asked questions
Is pre-shipment inspection mandatory?
That depends on the product, destination, contract, buyer requirements, and applicable trade controls. Even when it is not formally required, buyers may use PSI as a contractual quality-control measure. Product-specific legal or conformity requirements should be verified separately for the intended market.
Does a passed inspection guarantee that the entire order is defect-free?
No. A sampled inspection provides evidence about the inspected lot but does not prove that every unit is conforming. The level of assurance depends on the sampling plan, the quality of the specifications, access to the goods, and the inspection method.
Who should select the inspection samples?
The inspector should select samples randomly from the available finished goods. Supplier-prepared samples may not represent the overall shipment.
Can PSI replace supplier qualification?
No. Supplier qualification evaluates whether a supplier has the capacity and controls to meet requirements consistently. PSI checks a specific order near the end of production. Strong procurement uses both controls where the commercial risk justifies them.
Is laboratory testing part of a standard PSI?
Not necessarily. Some basic tests can be performed on-site, while specialised characteristics require suitable laboratory methods. Buyers should specify laboratory testing separately when the product or destination market requires it.
Should buyers pay the supplier before inspection?
Payment milestones should be negotiated in the purchase contract. Where commercially feasible, linking final payment or shipment release to an acceptable inspection result gives the buyer more leverage to address nonconformities before dispatch.
Prepare the order before you book the inspection
A successful PSI begins with a precise purchase order, measurable specifications, an approved reference sample, product-specific defect definitions, and clear decision rules. International buyers seeking structured sourcing and trade support can contact Hoorban to discuss the product, supplier location, documentation, inspection scope, and shipment requirements for their transaction.